Why Choose Bright Red PE Masterbatch for Global Sourcing?
Global sourcing demands more than a vivid red appearance. It requires repeatable shade control, stable processing, and dependable supply across different production sites. Bright Red PE Masterbatch can support these goals when its pigment system, carrier resin, and dispersion quality are carefully evaluated. A clean red pellet should feed smoothly, disperse evenly, and produce consistent color across film, injection-molded parts, and blown packaging.
Dr. Elena Marquez, a polymer color specialist, states, “Reliable color begins with controlled dispersion, not with brightness alone.” This principle matters during supplier comparisons. A sample may look excellent under showroom lighting, yet show blue or yellow shifts under daylight. That weakness can become costly during a long production run. Buyers should request laboratory data, recommended let-down ratios, heat-stability results, and batch-to-batch color records. They should also inspect pellet uniformity and packaging protection.
Practical experience matters here. I would not approve a supplier from one attractive sample alone. Production trials reveal more. Check feeding behavior, screen-pack pressure, surface streaks, and final color after cooling. Small differences can expose larger process problems.
Cost still matters. However, the cheapest Bright Red PE Masterbatch may create waste, rejected rolls, or repeated adjustments. That calculation is easy to miss. A reliable supplier should communicate clearly, document changes, and provide traceable technical support. Regional availability can shorten lead times, but it does not replace quality control. Global buyers need both. Even then, no sourcing decision is perfect; resin variation, equipment differences, and lighting conditions require ongoing review.
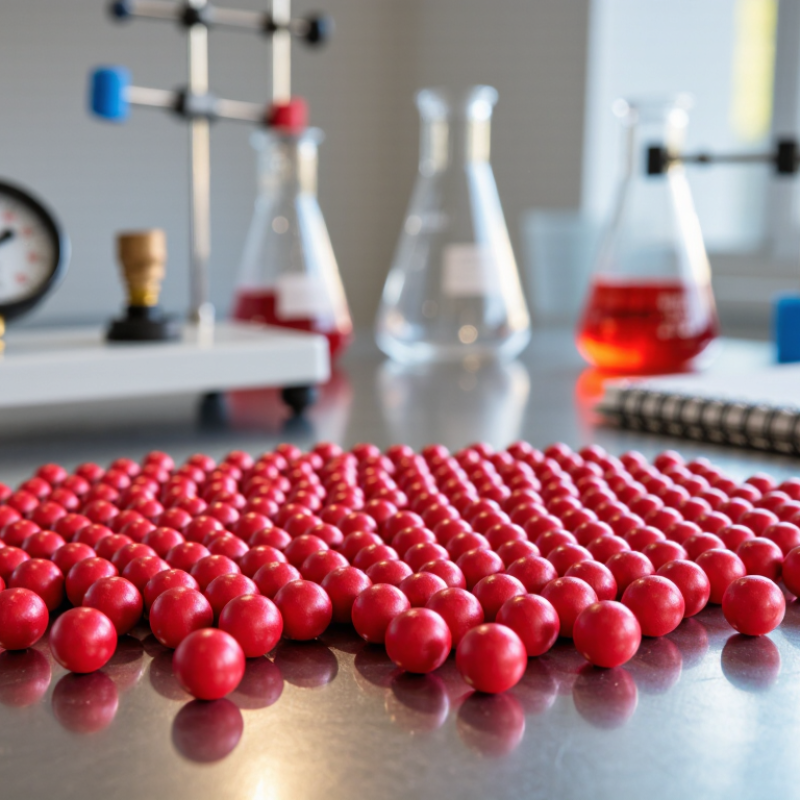
Bright red PE masterbatch is a concentrated color additive for polyethylene products. It contains red pigments dispersed in a polyethylene carrier resin. Manufacturers blend these colored pellets with natural PE during extrusion, injection molding, or blow molding. The heat melts the carrier and distributes the pigment through the polymer.
It is not simply red powder. Good dispersion matters. Poorly mixed pigment may create streaks, dark spots, or uneven color around bottle corners. A typical production check includes melt flow, pigment concentration, moisture, and compatibility with the chosen PE grade. The correct dosage depends on the product thickness, processing temperature, and required shade. Small trials are essential.
A bright red sample can look perfect under showroom lighting. It may appear different in daylight. I would compare molded samples under controlled light and inspect several production cycles. Color matching is rarely perfect on the first attempt. That is worth admitting. Buyers should request technical data, safety documentation, batch consistency records, and samples before global sourcing. They should also confirm whether the pigment and final application meet destination-market requirements, especially for packaging or other regulated uses. A reliable supplier should explain recommended processing conditions instead of offering color alone.
Bright red PE masterbatch depends on more than pigment strength. It requires controlled dispersion, stable carrier resin, and repeatable dosing. PlasticsEurope’s Plastics—the Fast Facts 2024 reports 54.6 million tonnes of plastics production in Europe during 2023. Such volume makes color variation expensive, especially across films, packaging parts, and molded components.
Consistency starts with measurable targets. Suppliers can define color using CIE L*a*b* values and control variation through ΔE calculations under ISO 11664-4 principles. ASTM D2244 also supports instrumental color-difference evaluation. A practical batch check should compare plaques made at the same let-down ratio, temperature, and cooling rate. The difference is visible.
Bright red pigments can reveal small process errors. Uneven feeding may create streaks. Excessive heat can reduce brightness. Moisture, incompatible additives, or poor dispersion can produce specks and cloudy areas. Experienced processors therefore check melt flow, pigment concentration, heat stability, and migration performance before approving production. Global sourcing also benefits from retain samples and agreed color tolerances.
Visual approval alone is not enough. A sample may look correct under warehouse lighting but shift under daylight. That limitation deserves honesty. Suppliers should provide batch records, test conditions, and recommended processing windows. Buyers should request trial runs using their actual PE grade. Small differences remain possible, but disciplined testing makes them manageable.
Why Choose Bright Red PE Masterbatch for Global Sourcing?
Bright red PE masterbatch supports reliable color production across films, bags, pipes, and molded packaging. Its concentrated pigment reduces handling volume and simplifies dosing during large production runs. A well-dispersed grade helps prevent streaks, specks, and uneven red tones. These defects are costly when containers leave the factory.
For global plastic manufacturing, consistency matters beyond color. Stable heat performance can reduce shade changes during extrusion or molding. Compatibility with polyethylene also supports smoother processing and fewer unexpected deposits in equipment. In practice, suppliers should provide technical data, safety documents, batch details, and quality certificates. These records improve traceability between shipments and support local regulatory reviews. They do not replace compliance checks.
Tips: Test the masterbatch with your exact resin, machine, and processing temperature. Compare a small trial sample under daylight and production lighting. Check pigment loading, moisture, carrier compatibility, and recommended let-down ratios. A shade may still shift slightly between machines. That is normal enough to investigate, not ignore. Keep approved color plaques for future comparison. Clear communication about recycled content, additive packages, and packaging conditions also prevents avoidable sourcing problems. A lower purchase price can become expensive if dispersion is poor. Scrutinize the details.
Why Choose Bright Red PE Masterbatch for Global Sourcing?
How to Evaluate Quality, Compatibility, and Safety
Bright red PE masterbatch should be judged by performance, not appearance alone. A vivid pellet can still create weak dispersion or unstable color. Ask for a current certificate of analysis, safety data sheet, and batch-specific technical data. Check pigment concentration, carrier resin, moisture, ash, and melt flow rate. Color can lie.
During sourcing trials, mix the masterbatch with the actual polyethylene grade and production equipment. Record the let-down ratio, extrusion temperature, screw speed, and cooling conditions. Examine molded plaques for streaks, specks, shade variation, and surface defects. Measure color difference with a spectrophotometer when repeatability matters. A small sample may perform well, yet larger batches can reveal feeding problems. Test it properly.
Compatibility deserves close attention. A PE-based carrier usually suits polyethylene applications, but additives, recycled content, and processing temperatures may change the result. Review heat stability, light resistance, migration data, and odor before approving production. For packaging or other regulated uses, confirm that the formulation meets the requirements of the destination market. Do not rely on a generic compliance statement. Request supporting test methods and applicable limits. I have found that supplier documentation is useful, but independent verification remains worthwhile. One overlooked detail, such as poor sealing after coloring, can become an expensive production issue.
| Evaluation Category | Key Indicator | Practical Target or Acceptance Criteria | Recommended Verification Method | Global Sourcing Considerations |
|---|---|---|---|---|
| Color Quality | Color strength and shade consistency | The supplied lot should match the approved color standard within the agreed color tolerance. A common instrumental control is ΔE, with the exact limit defined by the final product and color system. | Measure molded plaques or extruded film with a calibrated spectrophotometer under a documented illuminant and observer condition. | Request a retained color standard, lot sample, and certificate of analysis. Do not judge shade from pellets alone because molding conditions can change the appearance. |
| Color Quality | Pigment dispersion | No visible streaks, specks, agglomerates, or uneven coloration at the agreed let-down ratio. Dispersion should remain stable during the intended processing cycle. | Prepare a film, plaque, or extrudate at the production let-down ratio and inspect under controlled lighting. Microscopic dispersion testing may be used for critical applications. | Evaluate samples on the same or similar polyethylene grade and processing equipment used in production. |
| Carrier Compatibility | Polyethylene carrier suitability | The carrier should be based on a polyethylene grade compatible with the application resin, such as LDPE, LLDPE, HDPE, or a specified blend. | Review the technical data sheet and compare carrier type, melt flow characteristics, density, and recommended processing temperature with the base resin. | A PE carrier generally reduces compatibility risk in PE film, injection molding, blow molding, and extrusion applications, but compatibility must still be validated in the actual formulation. |
| Processing Performance | Recommended let-down ratio | Use the supplier’s validated dosage range, commonly expressed as a percentage of masterbatch in the final polymer. The optimum dosage depends on pigment loading, opacity requirements, and product thickness. | Run a dosage ladder, for example at 1%, 2%, 3%, and 5%, then compare color strength, dispersion, mechanical properties, and cost per finished kilogram. | A higher pigment concentration can reduce freight and storage volume, but it may require stronger mixing and tighter dosing control. |
| Processing Performance | Thermal stability | The pigment and carrier should withstand the actual residence time and processing temperature without significant color shift, degradation, plate-out, or odor. | Conduct a controlled heat-history test at the intended processing temperature and compare initial and aged color values. | Ask for the recommended processing temperature range and maximum continuous exposure guidance. Test separately for film, injection, blow molding, and extrusion processes. |
| Physical Properties | Moisture and pellet condition | Pellets should be free-flowing, clean, and substantially free from visible fines, foreign matter, and moisture-related clumping. | Inspect packaging and pellets visually; determine moisture using a validated laboratory method suitable for polymer additives. | Use moisture-barrier packaging where necessary and define packaging integrity, palletization, and storage conditions in the purchase specification. |
| Product Performance | Mechanical and functional impact | The masterbatch should not cause unacceptable changes in tensile strength, elongation, impact resistance, seal performance, stiffness, or transparency for the intended product. | Compare a control resin with colored samples at the production dosage using the relevant finished-product tests. | Bright red pigment systems can affect opacity and light transmission. Test both appearance and functional properties rather than color alone. |
| Safety and Compliance | Restricted substances and regulatory status | The formulation should comply with the laws and customer requirements applicable in the destination market, including restrictions on heavy metals, certain aromatic amines, phthalates, and other controlled substances where relevant. | Review a current compliance declaration and, for critical markets or applications, obtain independent laboratory test reports using recognized analytical methods. | Compliance is application- and market-specific. Define the destination countries and end use before approving the formulation. |
| Safety and Compliance | Food-contact suitability | For food packaging or articles, every component must be suitable for the intended food-contact use, conditions, and jurisdiction. A general “non-toxic” statement is not sufficient. | Request a food-contact declaration covering the pigment, carrier, additives, and use conditions; verify against applicable regional regulations and migration limits. | Do not assume that a color masterbatch is food-contact compliant merely because the carrier is polyethylene. |
| Safety and Compliance | Safety Data Sheet and hazard communication | A current Safety Data Sheet should identify hazards, handling, storage, spill response, disposal guidance, and relevant transport information in the required local language or format. | Check revision date, composition disclosure requirements, hazard classification, emergency information, and consistency with the product label. | Ensure documents are available for customs, warehouse, production, and occupational-safety teams in the importing country. |
| Quality Assurance | Lot-to-lot traceability | Each shipment should have a unique lot number linked to raw materials, production records, test results, packaging date, and release approval. | Audit the supplier’s quality records and verify that the lot number appears consistently on bags, cartons, certificates, and shipping documents. | Traceability supports faster investigation of color variation, contamination, customs questions, and customer complaints. |
| Quality Assurance | Certificate of Analysis (CoA) | The CoA should state the lot number, production date, test items, specification limits, actual results, and release status. | Compare the CoA with the purchase specification and independently test key attributes such as color, moisture, dispersion, and pellet appearance. | Agree in advance which tests are mandatory for every lot and which are verified periodically. |
| Supply Reliability | Packaging, shelf life, and storage | Packaging should protect pellets from moisture, contamination, and damage. Shelf life and recommended storage conditions should be clearly stated by the supplier. | Inspect packaging construction, seals, labels, storage instructions, and the condition of samples after simulated transport or storage. | Confirm whether temperature-controlled transport is necessary and apply first-in, first-out inventory management. |
| Commercial Evaluation | Total landed cost | Evaluate cost per unit of finished colored product, not only the price per kilogram of masterbatch. | Calculate: masterbatch price × dosage + freight + duties + testing + storage + scrap or conversion losses. | A concentrated, well-dispersed product may provide a lower total cost even if its purchase price per kilogram is higher. |
| Commercial Evaluation | Approval and change-control process | Any change to pigment, carrier, additive package, manufacturing site, or specification should require prior notification and approval. | Include a written change-control clause and require representative samples before commercial implementation. | This is especially important for multinational supply chains where an unnoticed formulation change can affect regulatory status or color matching. |
Why Choose Bright Red PE Masterbatch for Global Sourcing?
Bright red PE masterbatch can simplify color control across films, bags, pipes, and molded packaging. For international buyers, shade consistency matters more than a dramatic sample panel. Request a technical data sheet, safety documentation, and a recent certificate of analysis before discussing volume. Check pigment loading, carrier resin compatibility, recommended dosage, and melt-flow behavior. A small production trial often reveals problems that laboratory samples hide.
Ask suppliers to send sealed samples from the intended production batch. Compare them under standard daylight and your actual processing temperature. Keep reference plaques for future inspections. Packaging also deserves attention. Moisture-resistant bags, clear batch labels, and pallet stability reduce warehouse confusion. They matter during long ocean journeys. Confirm minimum order quantities, production lead times, and spare capacity before placing a seasonal order. A delayed red additive can stop an otherwise ready production line.
Freight terms need careful reading. Clarify whether prices include export handling, inland transport, insurance, or destination charges. Prepare commercial invoices, packing lists, certificates of origin, and product classifications early. Customs requirements can differ between countries and may change. Do not rely only on a supplier’s old paperwork. A low unit price can look attractive. It can also mislead. Currency movement, port congestion, and inspection delays may increase the landed cost. Some buyers overlook this. That mistake is expensive. Ask for a realistic delivery schedule, then add a modest buffer for unexpected disruptions.
It supports plastic films, bags, pipes, and molded packaging. The concentrated pigment reduces handling volume. Small trials matter.
Good dispersion helps prevent streaks, specks, and uneven red tones. These defects may appear when products leave the factory. Poor dispersion can increase waste and cleaning time.
Test the masterbatch with the exact resin, machine, and processing temperature. Compare samples under daylight and production lighting. Keep approved color plaques for later inspections.
Request technical data sheets, safety documents, batch details, and quality certificates. Check pigment loading, carrier compatibility, moisture, and recommended dosage. Do not rely only on old paperwork.
Yes, extrusion and molding temperatures can affect color stability. Different machines may produce slight shade changes. That is normal enough to investigate, not ignore.
Confirm minimum order quantities, production lead times, and spare capacity. Ask for sealed samples from the intended production batch. A seasonal order needs realistic planning.
Moisture-resistant bags help protect the material during storage and shipping. Clear batch labels reduce warehouse confusion. Stable pallets matter during long ocean journeys.
Review export handling, inland transport, insurance, destination charges, currency movement, and inspection delays. Port congestion may also increase delivery time. Details decide costs.
Commercial invoices, packing lists, origin certificates, and product classifications may be required. Requirements can differ between countries and change over time. Compliance checks remain necessary.
Not necessarily. Poor dispersion, delayed delivery, or extra freight charges can raise the landed cost. I would compare total cost, not just the quoted price. That assumption fails.
Bright Red Pe Masterbatch is a concentrated color additive designed to produce vivid, uniform red shades in polyethylene-based plastic products. When properly dispersed, it helps manufacturers achieve consistent color from batch to batch while reducing the risk of streaks, uneven tones, or excessive pigment use. Its performance depends on pigment quality, carrier resin selection, dispersion technology, and compatibility with the intended PE processing method, including film, molding, extrusion, or injection applications.
For global plastic manufacturing, this masterbatch can improve production efficiency, simplify color management, and support attractive, repeatable product finishes. International buyers should evaluate shade accuracy, thermal stability, dispersion, additive compatibility, packaging integrity, and relevant safety documentation before purchasing. They should also consider minimum order quantities, lead times, sample testing, transport conditions, customs paperwork, and supplier communication. A careful sourcing process helps ensure that Bright Red Pe Masterbatch arrives in reliable condition and performs consistently across different production environments.