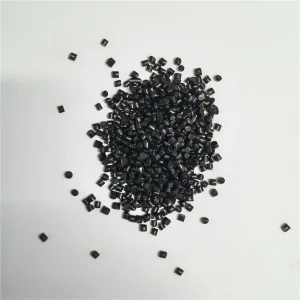
Direct factory-grade high-concentration colorants and additives engineered for synthetic bulk apparel, blown films, and extrusion applications.
In the rapidly evolving global trade landscape of 2026, enterprise buyers seeking Custom Bulk Apparel Suppliers & Supplier networks are no longer searching merely for transactional garment cutting and sewing facilities. Modern search intent mining reveals a profound shift toward total vertical integration—encompassing primary polymer compounding, synthetic yarn dope-dyeing (spin dyeing), performance fiber additive masterbatch chemistry, and Industry 4.0 smart manufacturing resilience.
As global sustainability mandates like the EU Corporate Sustainability Due Diligence Directive (CSDDD) take full effect, procuring apparel at scale requires an audit-proof paper trail spanning raw material purity, thermal processing stability up to 260°C, zero-water coloration technology, and strict chemical safety standards (REACH, RoHS, and OEKO-TEX Standard 100). Changzhou Jiazhou Plastic Products Co., Ltd., leveraging 16 years of specialized manufacturing experience across a 6,000m² state-of-the-art facility, stands at the nexus of high-end raw material formulation and bulk textile supply chain integration.
Traditional bulk apparel buyers frequently suffer from batch-to-batch color variance (high Delta E values), premature UV degradation in outdoor activewear, and environmental penalties associated with high-polluting wet dye houses. Our whitepaper demonstrates that true supply chain excellence begins at the molecular level. By utilizing high-concentration polyethylene (PE) and polypropylene (PP) carrier masterbatches enriched with nano-dispersed organic and inorganic pigments, custom apparel producers achieve flawless color fastness, zero liquid effluent pollution, and superior tensile strength retention during high-speed synthetic fiber melt-spinning.
When global procurement directors evaluate Custom Bulk Apparel Suppliers & Supplier networks, their intent is governed by strict quantifiable criteria. Below is the decision framework utilized by Fortune 500 apparel brands and high-volume industrial wear procurement teams:
Demanding a Spectrophotometer Delta E < 0.5 across production lots. Utilizing twin-screw extruders to ensure pigment agglomerates are reduced below 5 microns, eliminating fiber breakage during high-speed spinning of synthetic bulk garments.
High-temperature processing capability up to 260°C without color shade shifting, sublimation, or polymer degradation, ensuring compatibility with synthetic extrusion, melt-blown non-wovens, and injection-molded garment accessories.
Full audit compliance with heavy-metal-free, non-toxic formulations meeting EU REACH Annex XVII, SVHC candidates list, RoHS, and food-contact safe standards for next-to-skin activewear and medical bulk apparel.
The future of bulk apparel manufacturing relies heavily on material science breakthroughs that replace traditional post-weaving dyeing with mass-pigmentation during polymer compounding. Below is our engineering roadmap for next-generation bulk apparel raw materials:
Transitioning from conventional fossil-based PE/PP carriers to bio-based PolyLactic Acid (PLA) and Polyhydroxyalkanoates (PHA) masterbatches derived from agricultural waste, achieving a 65% reduction in cradle-to-gate carbon footprint.
Combining color pigments with functional micro-encapsulants—including permanent anti-static agents, anti-microbial silver ion matrices, and infrared-reflecting cool-touch particles for performance outdoor sportswear.
Engineering specialized carrier chemistry designed specifically to bond with post-consumer recycled PET flakes, ensuring uniform color intensity without compromising filament tensile elongation.
Different apparel and industrial textile sectors demand customized material properties. Our comprehensive product portfolio addresses specific vertical industry challenges:
Industrial protective apparel requires extreme color retention under repeated industrial laundering and UV exposure. By compounding high-concentration PE yellow and blue masterbatches with specialized Hindered Amine Light Stabilizers (HALS), we guarantee that safety apparel complies with ISO 20471 high-visibility standards over extended operational lifespans.
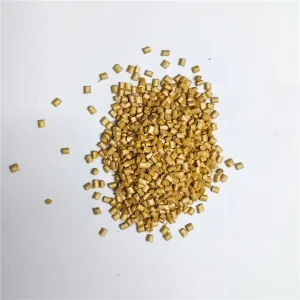
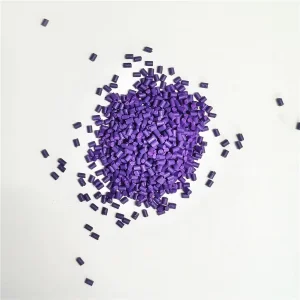
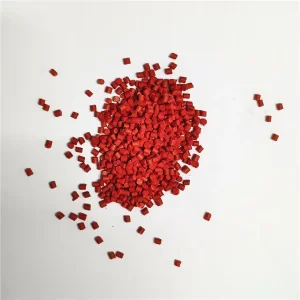
Modern sportswear brands demand non-migrating, anti-fading color formulations that do not bleed under high-perspiration conditions. Our custom PE gold, silver, rose red, and purple masterbatches feature ultra-fine dispersion, allowing micro-filament extrusion (down to 1.0 denier per filament) without spinneret clogging or thread snapping.
In addition to wearable garments, bulk apparel suppliers require heavy-duty packaging films and protective non-woven bags. Our high-opacity black and white PE masterbatches deliver exceptional covering power and heat sealing strength for e-commerce logistics packaging and apparel dust covers.
Situated in Changzhou, Jiangsu Province—the core manufacturing heartland of Eastern China—Changzhou Jiazhou Plastic Products Co., Ltd. embodies the efficiency, scale, and technical precision of Industry 4.0 modular manufacturing.
High-speed continuous mixing extruders equipped with loss-in-weight gravimetric feeders guarantee exact pigment loading ratios, eliminating batch variations and reducing raw material waste by 14%.
Integrated raw material buffer stock combined with proximity to Shanghai and Ningbo deep-water ports allows standard order fulfillment cycles to be compressed to 15 days from PO confirmation to container loading.
Every batch undergoes rigorous quality assurance including Melt Flow Index (MFI) testing, ash content analysis, filter pressure value (FPV) assessment, and Xenon arc weatherometer lightfastness testing.
Exporting bulk apparel and synthetic raw materials to strict regulatory regions like North America, the European Union, and East Asia requires absolute compliance with local environmental and consumer safety legislation.
Guaranteed zero phthalates, heavy metals (lead, cadmium, hexavalent chromium), or restricted aromatic amines, ensuring seamless customs clearance across all EU member states.
Fully traceable masterbatch formulations designed to blend homogeneously with GRS-certified recycled polyolefins and polyester resins, aiding brands in achieving zero-carbon milestones.
Dedicated color technicians provide fast 48-hour lab dip matching based on Pantone, RAL, or physical target swatches provided by international buying offices.
Below is the comprehensive engineering datasheet for our core PE masterbatch series engineered for synthetic fiber extrusion, blown film, and injection-molded apparel accessories:
| Masterbatch Grade | Carrier Resin | Pigment Load (%) | Heat Resistance | Light Fastness (Blue Wool) | Key Target Application |
|---|---|---|---|---|---|
| PE Silver Masterbatch | LLDPE / LDPE | 35% Metallic Pigment | 260°C | Grade 7-8 | Metallic Activewear, Decorative Trims |
| PE Gold Masterbatch | LDPE / HDPE | 40% Premium Luster | 260°C | Grade 7-8 | Luxury Apparel Packaging, Accessories |
| PE Black Masterbatch | HDPE / LLDPE | 50% High-Surface Carbon Black | 280°C | Grade 8 | High-UV Outdoor Wear, Logistics Bags |
| PE White Masterbatch | LDPE / PP | 70% Anatase/Rutile TiO₂ | 260°C | Grade 8 | Opaque Protective Apparel, Medical Sheets |
| PE Red / Blue / Yellow | PE Carrier | 30% - 45% Organic Pigment | 260°C | Grade 6-7 | Sportswear, Custom Bulk Apparel Fibers |
Dope dyeing (adding masterbatch pellets directly into the polymer melt prior to fiber extrusion) eliminates the need for liquid water dye baths. This process reduces water consumption by up to 90%, lowers energy utilization by 60%, and results in vastly superior color fastness to washing, rub resistance, and UV light exposure compared to post-woven piece dyeing.
For high-concentration masterbatches, typical let-down ratios range from 1% to 4% by weight, depending on the required opacity, fiber denier, and color intensity. Our technical team provides precise dosing calculations to optimize cost per kilogram while maintaining mechanical tensile strength.
Yes. Our high-concentration PE masterbatch grades are thermally stabilized up to 260°C (and up to 280°C for specialized black grades). This ensures that color molecules do not degrade, gas off, or shift hue during heat setting, extrusion, or ultrasonic welding of synthetic garments.
Absolute compliance is our top priority. All our products are formulated using non-toxic, heavy-metal-free pigments and food-grade polyethylene carriers. They comply fully with EU REACH SVHC, RoHS, and FDA guidelines for next-to-skin contact and food packaging.
Our standard MOQ for stock masterbatch formulations is 500 kg. For custom color matching, lab dips are generated within 48 hours, and bulk production is completed within 10 to 15 business days from sample approval.
We maintain dual raw-material sourcing channels for titanium dioxide, carbon black, and organic pigments to shield clients from raw material price volatility. Additionally, our automated 6,000m² factory operates under ISO 9001:2015 quality protocols, guaranteeing batch consistency year-round.
Browse our factory-direct product lines engineered for global plastic processors, textile fiber extruders, and custom bulk apparel manufacturers.