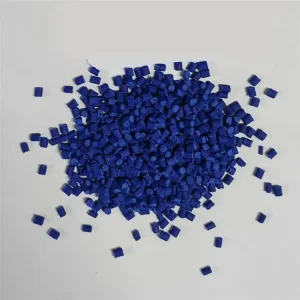
Namibia Agritech High Concentration Blue Masterbatch PE Carrier
Explore Specification
Targeted thermal-stability formulations designed for Namibia's aggressive UV profile, high daytime ambient processing, and agricultural grade blow-film requirements.
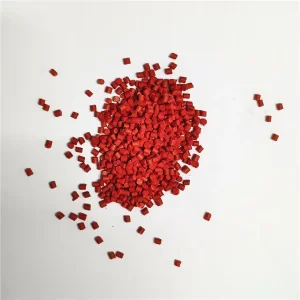
The manufacturing and polymer transformation sector in Namibia—concentrated in key logistics and industrial epicenters like Windhoek, Walvis Bay, and Swakopmund—is undergoing accelerated modernization. Driven by expanding municipal infrastructure, agricultural automation, and regional logistics corridor connectivity across the SADC (Southern African Development Community), polymer processors require compounding additives engineered beyond standard commercial tolerances.
Namibia's distinctive geographical profile presents rigorous technical challenges: extreme ultraviolet (UV) radiation indices exceeding Level 11, expansive diurnal temperature fluctuations ranging from freezing desert nights to sub-tropical midday peaks, and hyper-saline coastal corridors around Erongo. In blow-molding and extrusion lines, ordinary pigments degrade prematurely, causing polymer chalking, chain-scission brittleness, and chromatic drift. Our direct supply channel delivers polymer-specific chemical stabilization, offering superior dispersion kinetics and antioxidant synergy tailored precisely to local processing demands.
Leveraging twin-screw compounding automation, spectrophotometric real-time monitoring, and intelligent supply scheduling to eliminate lead-time bottlenecks.
Our intelligent factory lines continuously measure melt flow index (MFI) and shear viscosity in real time, preventing nozzle clogs and film bubbling during high-speed extrusion lines operating in Namibia conversion facilities.
Utilizing co-rotating intermeshing screws with customized shear-element configurations ensures nano-pigments and calcium carbonate (CaCO₃) achieve complete surface wetting, eradicating visual agglomerations in blown films under 15 microns.
With integrated logistics planning, sea cargo transit from our production lines through the Port of Walvis Bay reaches distribution warehouses in under 28 operational days, cutting safety buffer requirements for African plastics converters.
Tailored formulations designed to enhance mechanical properties, reduce raw material costs, and ensure absolute compliance with global environmental standards.
Namibia’s arid environment demands robust water retention and drip-irrigation infrastructure. Our high-concentration black masterbatch delivers high carbon dispersion with optimized particle diameter, protecting HDPE and LLDPE water pipes against severe environmental stress cracking (ESCR) and subterranean biological deterioration.
For supermarket carriers, courier polybags, and agricultural mulch film manufacturing in Namibia, our high-opacity white and specialty color masterbatches provide superior hiding power at lower addition ratios (1% to 3%), significantly decreasing cost-per-ton without sacrificing tensile or dart impact strength.
Strictly manufactured under ISO 9001 and ISO 14001 compliance standards, delivering reproducible batch integrity across all thermal and chromatic profiles.
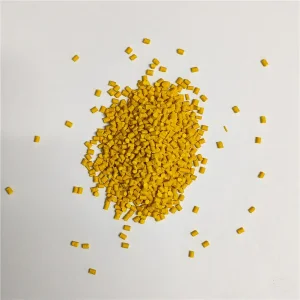
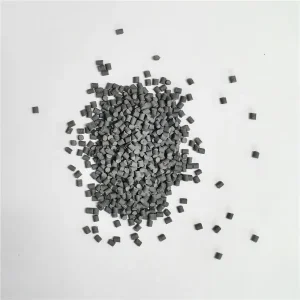
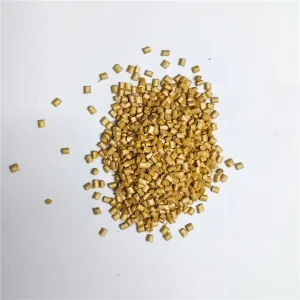
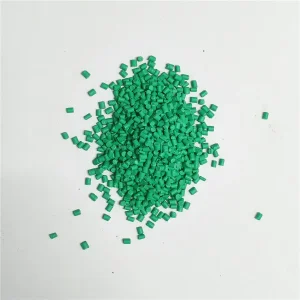
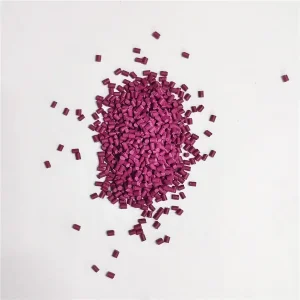
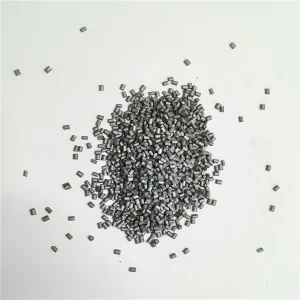
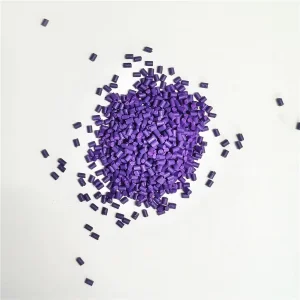
Complete documentation packages engineered for hassle-free clearance through Namibian Revenue Agency (NamRA) checkpoints.
Every masterbatch batch leaves our plant certified free of toxic heavy metals, lead chromates, and hazardous phthalates—ensuring full alignment with strict Southern African environmental conservation initiatives.
We provide full pre-shipment documentation sets, including verified Certificates of Analysis (COA), HS Code standardization, and cargo declarations to expedite direct processing at Walvis Bay container terminals.
Our remote polymer chemistry team delivers customized formulation adjustments, troubleshooting extrusion melt-fractures, pigment streaking, and thermal degradation via direct real-time video telemetry.
Comprehensive answers addressing lead times, carrier resin compatibility, minimum orders, and thermal resistance tolerances.
Production typically requires 7 to 15 business days depending on custom color matching. Ocean freight via international container shipping from Ningbo/Shanghai to the Port of Walvis Bay requires approximately 28 to 35 days, providing a predictable delivery window for Namibian converters.
Every single batch undergoes rigorous testing using computer spectrophotometers, Melt Flow Index (MFI) testers, and blown-film test extruders. We maintain internal chromatic tolerances under ΔE < 0.2, ensuring absolute color consistency across recurring shipments.
Yes. Our PE and PP masterbatches utilize virgin polyolefin carrier resins with high molecular compatibility and specialized dispersion aids, designed to stabilize and homogeneously tint varied PCR blends without chain degradation or excessive screen pack clogging.
Standard color and black/white masterbatches start at a low MOQ of 500kg. For bespoke PANTONE/RAL color formulations tailored to Namibian commercial packaging brands, our baseline MOQ is 1,000kg with complimentary pilot lab-sample matching available beforehand.
Partner with an established manufacturer offering 16+ years of specialized compounding expertise, rigorous laboratory QA, and direct container delivery to Walvis Bay.
Send Inquiry Now